Select a country or region

Global

English

Industry challenges

Waste-liquid recovery is difficult and hazardous-waste disposal is costly

Mixed waste liquid after exhaust absorption is difficult to separate and purify

It can only be handled as hazardous waste

Organic solvents are wasted and disposal costs are high

Low purification accuracy and poor equipment adaptability

Traditional distillation produces low-purity solvent that cannot be reused directly

General distillation equipment has weak corrosion resistance, scales easily, and consumes much energy

Difficult to operate steadily with complex mixed-solvent conditions

Low automation and high labor costs

Traditional equipment depends on manual operation

Inaccurate parameter control makes purification efficiency unstable

High labor input

Our solutions

Related products

01

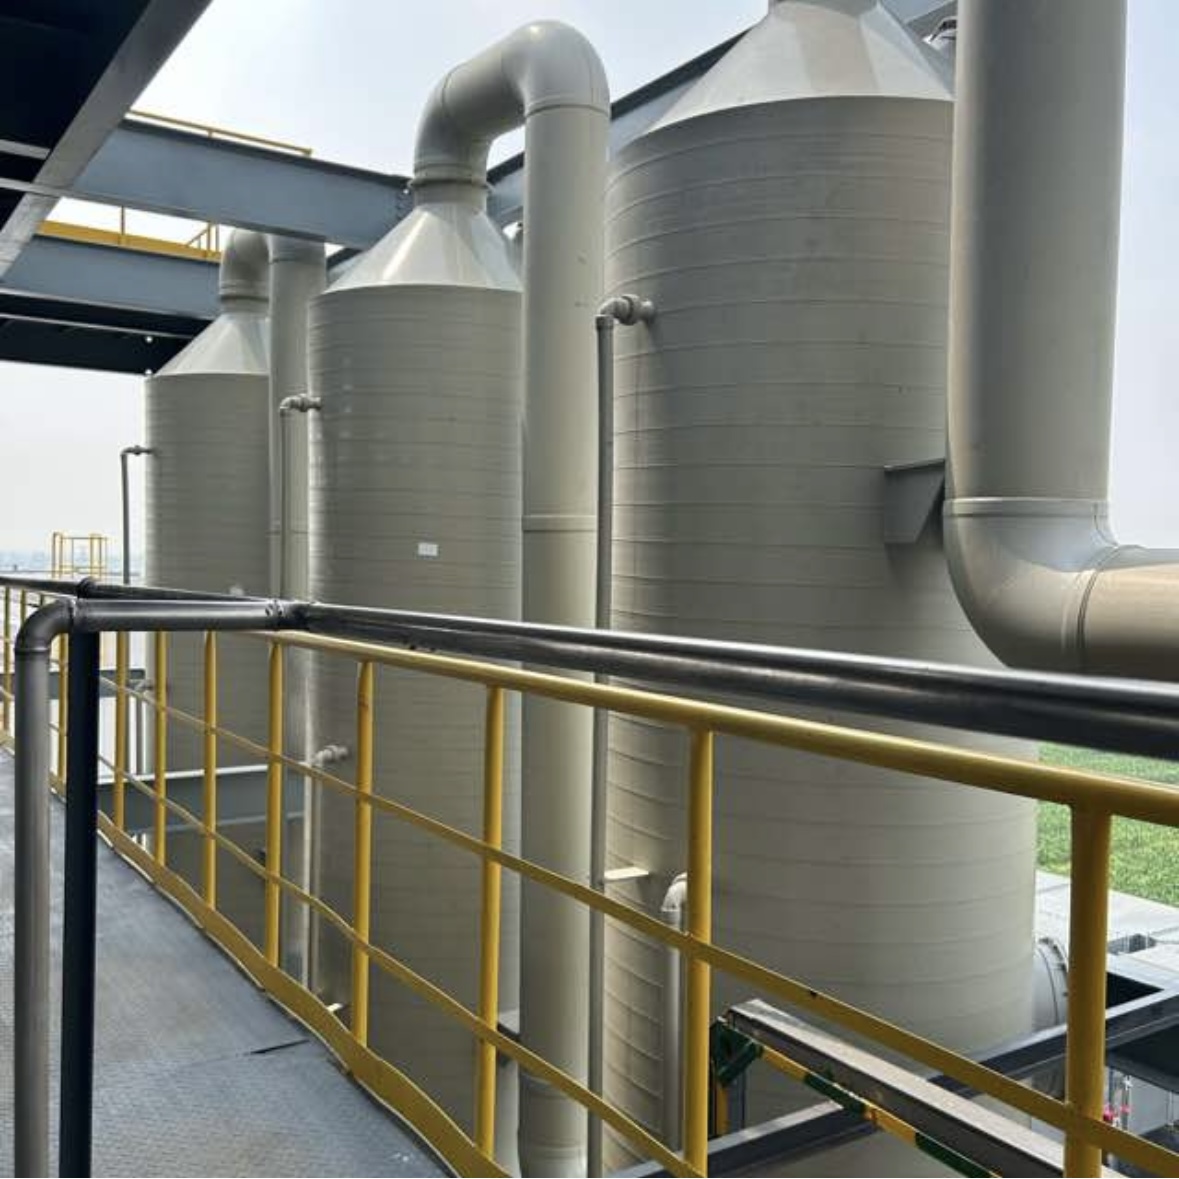
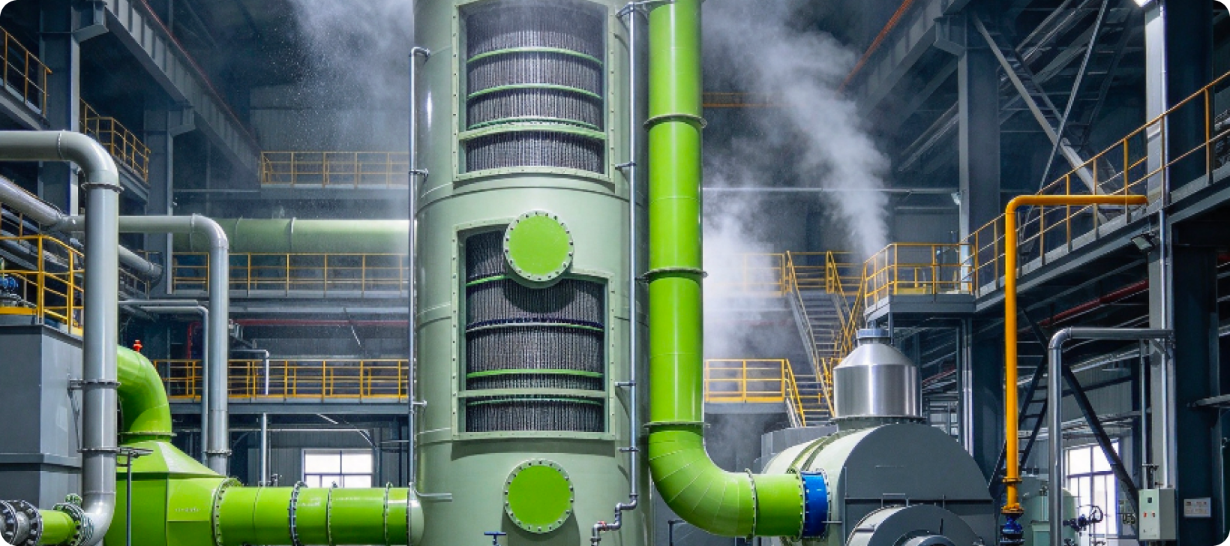
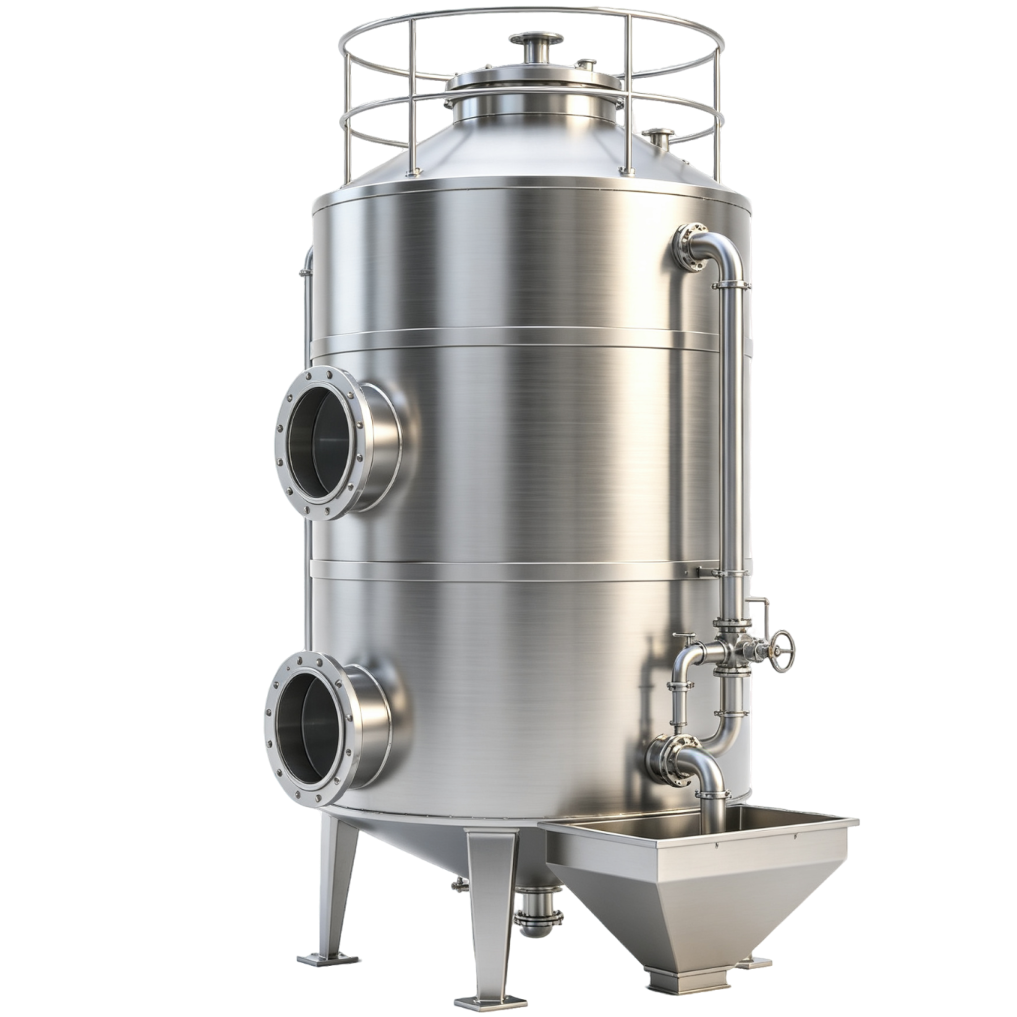
Stainless-steel spray tower

Through counter-current gas-liquid contact, the spray tower efficiently removes acidic and alkaline gases, water-soluble pollutants, and dust.

01

Stainless-steel spray tower

Through counter-current gas-liquid contact, the spray tower efficiently removes acidic and alkaline gases, water-soluble pollutants, and dust.

01

Stainless-steel spray tower

Through counter-current gas-liquid contact, the spray tower efficiently removes acidic and alkaline gases, water-soluble pollutants, and dust.

Manufacturing and servicesHow it works

01

Process-condition customization

According to solvent composition, boiling point, throughput, and purity requirements, we customize the distillation tower size, packing stages, and heating parameters.

02

Precision design

Use 3D modeling to optimize the tower structure, packing arrangement, and reflux system, maximizing distillation efficiency and purification accuracy.

03

Precision manufacturing

Use CNC tube rolling, seamless welding, and polishing to complete pressure, high-temperature, and airtightness tests for the tower, then install packing precisely.

04

Custom export packaging

Use dedicated moisture- and rust-resistant packaging and ship the equipment in sections for sea transport.

05

Installation and commissioning

Connect the equipment to the exhaust treatment system on site, adjust temperature, pressure, and reflux parameters, and deliver it after trial production meets the requirements.

06

Long-term after-sales support

Provide operation and maintenance guidance, packing cleaning and replacement, parameter optimization, upgrades, and lifetime technical support.

Get your tailored solution

Products you may be interested in

Spray tower

Activated-carbon adsorption tank

Biological deodorization tank

Absorption tower

Requirement customization

Request a quote

OEM customization

Technical support

Upload drawings/files

Submit

FAQs

We could not find what you need. Please contact our team.

View details

What solvent purity can the distillation tower achieve?

Depending on the solvent composition, purified solvent can reach 95%-99% purity, fully meeting production-line reuse requirements and greatly reducing raw-material purchasing costs.

Is the equipment energy-intensive, and what are the operating costs?

Intelligent precision temperature control and heat reuse keep energy consumption low. Automated operation needs no continuous attendance, so long-term benefits exceed operation and maintenance costs.

Can it process mixed waste liquid containing several organic solvents?

A multi-stage distillation process can be customized according to boiling-point differences and can purify mixed organic waste liquid containing esters, alcohols, ketones, hydrocarbons, and other solvents.

Is the equipment prone to scaling and blockage?

A smooth stainless-steel tower, high-voidage structured packing, and front-end filtration help prevent blockage, while the equipment remains easy to clean and maintain.

Contact us

If you have questions or need help, contact our team for dedicated support.

We look forward to hearing from you

Submit